Direct from our IATF 16949 & ISO 9001 certified manufacturing facilities in Xiamen, explore our core line of high-duty fluid pumping units designed for OEM kitchen appliances, thermal loops, smart sanitary ware, and commercial systems.
In modern structural plumbing and industrial architectural design, the global market for kitchen sink macerator pumps has evolved from a niche drainage workaround into a critical infrastructure component. Unlike standard sanitary sewage pumps handling soft human organic solids, kitchen sink wastewater presents one of the most mechanically and chemically aggressive fluid environments in the entire building envelope. It combines dense particulate food slurry, suspended fibrous vegetable waste, high-temperature cooking effluent reaching up to 90°C (194°F), and dynamic mixtures of grease, fats, oils, and chemical surfactants.
Historically, residential and commercial developers encountered prohibitive civil engineering costs when installing kitchen sinks in basements, converted industrial lofts, rooftop lounges, or central kitchen islands located far from the main gravity-fed soil stack. Breaking concrete foundations, trenching subfloors, and core-drilling load-bearing beams not only escalate structural costs exponentially but frequently violate structural safety codes. Custom kitchen sink macerator units solve this structural deadlock by pulverizing solid culinary residues down to microscopic fractions (under 3mm) and using high-head hydraulic impellers to discharge slurry vertically and horizontally through narrow-diameter pipes (DN25 to DN32).
According to recent global fluid mechanics and plumbing retrofit data, the demand for compact, high-duty greywater maceration systems is compounding at over 7.4% annually across North America, the European Union, Southeast Asia, and Australasia. This demand is accelerated by two distinct macro waves: the boom in adaptive reuse of commercial real estate (converting vacant office towers into residential micro-apartments and ghost kitchens) and consumer demand for flexible residential open-plan kitchen islands without cutting slab foundations.
However, legacy off-the-shelf macerators built around heavy AC induction motors and primitive dual-blade cutters suffer from severe chronic liabilities: thermal cut-outs when scalded by boiling pasta water, premature shaft seal leakage caused by acidic detergent corrosion, high operational acoustic noise exceeding 65 dB(A), and frequent motor stator burnout caused by fibrous food entanglement. These industry failures have compelled Tier-1 appliance OEMs and commercial kitchen brands to turn toward specialized custom pump manufacturers like RETO, demanding brushless DC (BLDC) motor platforms, food-grade mechanical face seals, and intelligent anti-blockage control logic.
The convergence of electronic motor commutation, fluid dynamic modeling, and connected sensing is driving an architectural revolution in greywater handling equipment.
Shifting from bulky AC induction motors to ultra-compact Brushless DC (BLDC) motors represents a massive paradigm shift. BLDC architectures eliminate friction-prone carbon brushes, allowing for variable PWM speed regulation, instantaneous high starting torque to shear fibrous debris, and energy reductions of up to 45%.
Kitchen sink pumps must endure acute thermal shocks from continuous boiling discharge while resisting animal fats, acidic sauces, and alkaline dish detergents. Contemporary trends deploy PPS (polyphenylene sulfide) impeller housings, silicon carbide (SiC) mechanical face seals, and Viton/FKM fluoroelastomers to guarantee a 10-year lifespan.
Modern high-end open-plan luxury homes demand virtually silent under-sink operation. Leading manufacturers incorporate internal elastomer suspension dampening, optimized hydraulic volute spiral geometries, and hermetically sealed rotor chambers to suppress cavitation resonance and acoustic propagation below conversational thresholds.
Traditional single-blade spinning disks frequently choke on vegetable fibers like celery, onion skins, and corn husks. State-of-the-art designs employ SUS316 or laser-hardened 440C stainless steel multi-tier cutting rings that combine rotary shears with progressive stationary teeth to reduce solids into a fluid-homogenized slurry.
Integrating intelligent micro-controllers within the pump PCB enables real-time motor current monitoring. If a hard bone or utensil causes rotor stall, the controller executes an instant reverse-pulse oscillating cycle (rocking motion) to dislodge the jam before safely shutting down and triggering an LED or audio diagnostic signal.
Under-sink real estate has become fiercely competitive due to the proliferation of RO water filters, instant boiling/chilling water dispensers, waste sorting bins, and pull-out organizers. Next-generation custom macerator designs feature ultra-low horizontal heights (sub-150mm) to fit snugly behind or underneath standard kitchen cabinetry base drawers.
Compare the hydraulic, thermal, and lifecycle parameters that OEM product engineers, plumbing contractors, and appliance system integrators examine when specifying kitchen sink macerators.
| Performance Dimension | RETO Custom BLDC Macerator Platform | Conventional AC Induction Macerator | Standard Brushed DC Greywater Pump |
|---|---|---|---|
| Motor Architecture | Electronically Commutated Brushless DC (BLDC) | Single-Phase Capacitor-Start Induction | Permanent Magnet Brushed DC (PMDC) |
| Continuous Service Life | > 35,000 Operating Cycles (Bearing-limited) | 8,000 – 15,000 Cycles (Thermal degradation) | 1,500 – 3,500 Hours (Carbon brush wear) |
| Acoustic Emission Level | 38 – 45 dB(A) (Whisper-quiet cabinet operation) | 58 – 68 dB(A) (Heavy mechanical rumble) | 52 – 62 dB(A) (High-pitch brush whining) |
| Continuous Fluid Temp Rating | Up to 90°C (Boiling water & dishwasher proof) | Typically max 50°C (Thermal trip risk) | Max 40°C – 45°C (Plastic deformation risk) |
| Starting Torque & Anti-Jam | 350% Peak Starting Torque + Dynamic Bi-Directional Rocking | Fixed torque; easily locked by fibrous food waste | Moderate starting torque; rapid motor burnout |
| Overall Volumetric Size | Ultra-Compact (Fits behind standard cabinet plinths) | Bulky, heavy casting (Consumes entire cabinet) | Medium, requires frequent service access |
| Control Interface & IoT | PWM speed control, FG tachometer output, CAN/LIN ready | Simple On/Off mechanical diaphragm switch | Analog on/off float or pressure switch |
| Electrical Efficiency | > 82% Motor Efficiency (Low power dissipation) | 45% – 55% Efficiency (Generates internal heat) | 50% – 60% Efficiency (Frictional brush losses) |
Custom kitchen sink macerators eliminate civil construction obstacles across diverse residential, commercial, maritime, and specialized institutional environments.
Transforming dark residential basements into luxurious in-law suites, entertainment wet bars, or supplementary kitchenettes requires overcoming the vertical gravitational drop. With up to 8–10 meters of vertical hydraulic lift, our macerators pump waste straight up through small concealed pipes to the municipal sewer line without sub-slab excavation.
High-rise penthouse condos and historic loft conversions frequently possess post-tensioned concrete slabs where drilling floor penetrations is structurally prohibited. A compact under-sink macerator routes waste up through the ceiling plenum or along interior partitions via 32mm discharge lines to the main riser effortlessly.
Shopping mall pop-ups, airport coffee bars, and commercial ghost kitchens produce massive volumes of spent coffee grounds, milk froth, and hot water rinses. Our high-torque multi-stage cutting pumps handle particulate coffee grit without clogging or impeller abrasive scoring, ensuring continuous commercial operation.
Space and power constraints are extreme in yachts, catamarans, and expedition recreational vehicles. RETO’s native 12V and 24V BLDC macerators deliver industrial shredding power directly from vehicle battery banks, handling organic galley food waste safely while operating quietly on off-grid DC circuits.
RETO's multidisciplinary R&D center is leading the engineering transition toward predictive, hermetic, and zero-maintenance fluid handling systems.
Integrating advanced Field Oriented Control (FOC) algorithms that detect mechanical viscosity changes in real time. The pump autonomously distinguishes between light soapy water and heavy organic sludge, dynamically scaling torque, impeller RPM, and active power consumption down to millisecond increments.
Transitioning to sealless, magnetically coupled macerator drive shafts. By completely isolating the electromagnetic motor stator from the wet fluid cavity using an engineered ceramic containment shroud, dynamic shaft seal degradation and liquid intrusion failures are eliminated entirely from the product lifecycle.
Integrating low-power ultrasonic transducers into the pump volute walls to shatter congealed culinary grease molecules before they adhere to internal pump surfaces. Coupled with IoT cloud telemetry, future pumps will provide building facility managers with predictive health analytics and automated descaling cycles.
A persistent pain point in under-sink wastewater pumping is sewer gas siphonage and backflow contaminated with bacteria. RETO engineers integrate dual spring-loaded EPDM non-return check valves directly into the discharge elbow, complemented by an internal activated-carbon air breather cartridge or dedicated vent connection that completely locks hazardous methane and sulfur odors inside the pumping chamber.
Contemporary kitchens rarely feature just a single sink bowl; installations encompass double basin sinks, integrated dishwashers, water softeners, and condensation lines from high-efficiency combi-boilers. Our custom macerator housings provide three to four distinct side-inlet ports with universal stepped rubber adapters (40mm, 32mm, 25mm), permitting simultaneous connection of multi-temperature waste feeds.
Leveraging our advanced automotive-grade production lines in Xiamen, RETO manufactures kitchen macerators with precision automation. Key manufacturing nodes—such as automated stator needle winding, automated high-pressure helium leak checks, 100% dynamic rotor balancing, and computer-vision dimensional verification—ensure failure rates under 50 PPM (parts per million).
Clearing customs and regional building code mandates is critical for multinational appliance brands. RETO products undergo independent lab testing to achieve TÜV certification, CE, RoHS, and REACH verification. Units meet plumbing hygiene standards such as EN 12050-2 for greywater lifting equipment and ASME A112.3.4 for macerating systems.
Direct engineering answers to the critical hydraulic, electrical, and structural inquiries encountered during OEM macerator specification.
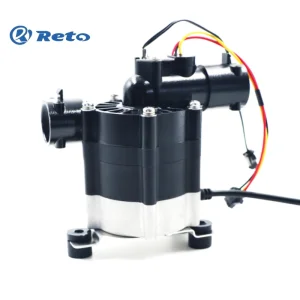
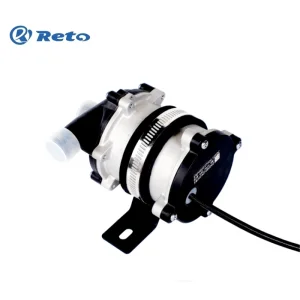
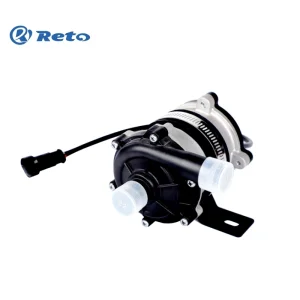
Complementing our kitchen sink macerators, RETO engineers world-class brushless DC pumps for smart sanitary appliances, new energy thermal loops, high-temperature hot water circulation, and compact booster platforms.
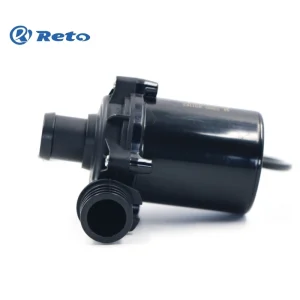
Partner directly with RETO’s specialized motor and hydraulic engineering teams in Xiamen, China. From initial 3D CAD modeling and finite element fluid analysis (FEA) to pilot tooling, lab validation, and volume delivery certified under IATF 16949 and ISO 9001.